In modern-day lab environments, the factory price large capacity refrigerated centrifuge is not just a separation apparatus—it is precision engineering. With simple-to-view digital displays and microprocessor controls, it makes it easy for scientists to quickly adjust variables like acceleration and deceleration rates. Other models come equipped with onboard diagnostics that analyze rotor condition and operating performance. High-end safety features like automatic lid interlocks and imbalance detection offer protection at every cycle. With more rapid and consistent processing needed in industries, factory price large capacity refrigerated centrifuge technology keeps up with stability, precision, and greater throughput capability.
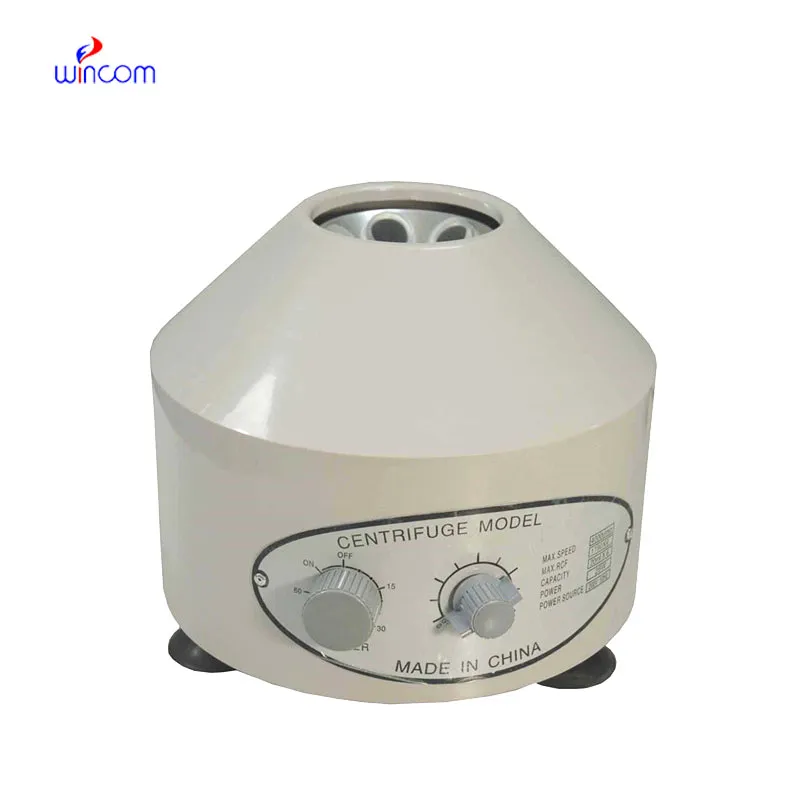
factory price large capacity refrigerated centrifuge technology is a principal component in diverse manufacturing processes. In wastewater treatment, factory price large capacity refrigerated centrifuge assist in separating sludge from liquids to improve recycling efficiency. In the manufacture of cosmetics, factory price large capacity refrigerated centrifuge facilitate even emulsion and cream mixing. Crop research facilities apply it to analyze soil nutrients and plant extracts. It is also used in the manufacture of vaccines through the purification of viral particles and protein fractions. Through the ability to adapt to many substances and work requirements, factory price large capacity refrigerated centrifuge continues to support industries seeking consistency, purity, and scalability.
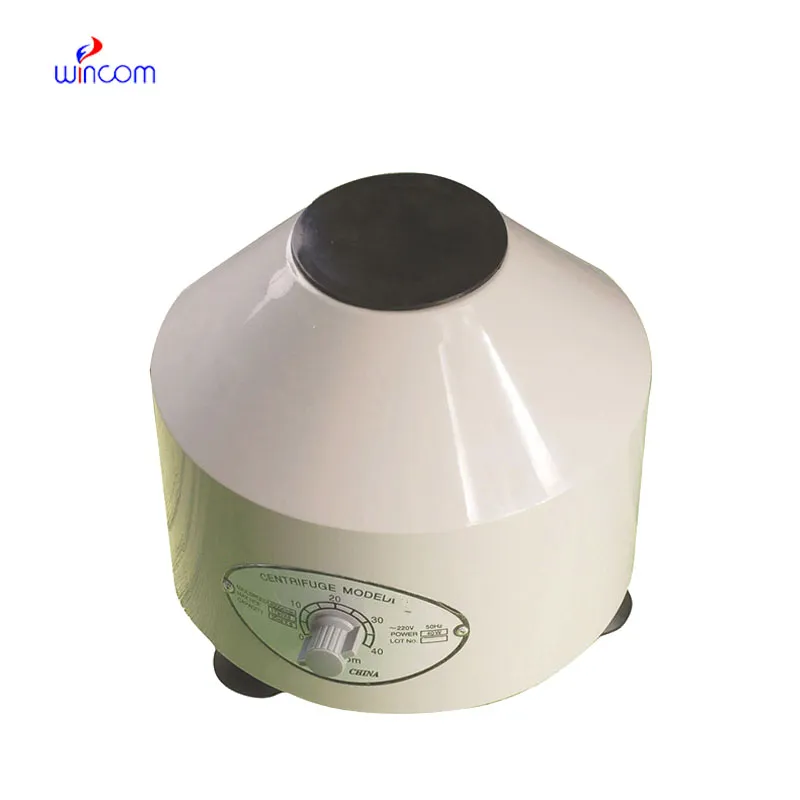
Advances in automation and material science will shape the future of factory price large capacity refrigerated centrifuge. Composite lightweight materials will offer increased speed and reduced mechanical stress. Integrated AI controls will streamline rotor performance and balance in real time. The addition of remote operation and touchless interfaces will increase accessibility in sterile environments. As data-driven laboratories expand, factory price large capacity refrigerated centrifuge will be connected to cloud-based systems for predictive diagnostics and performance analytics. All these innovations will create a new generation of smart instruments with the capacity to enable high-throughput, complex applications with precision.
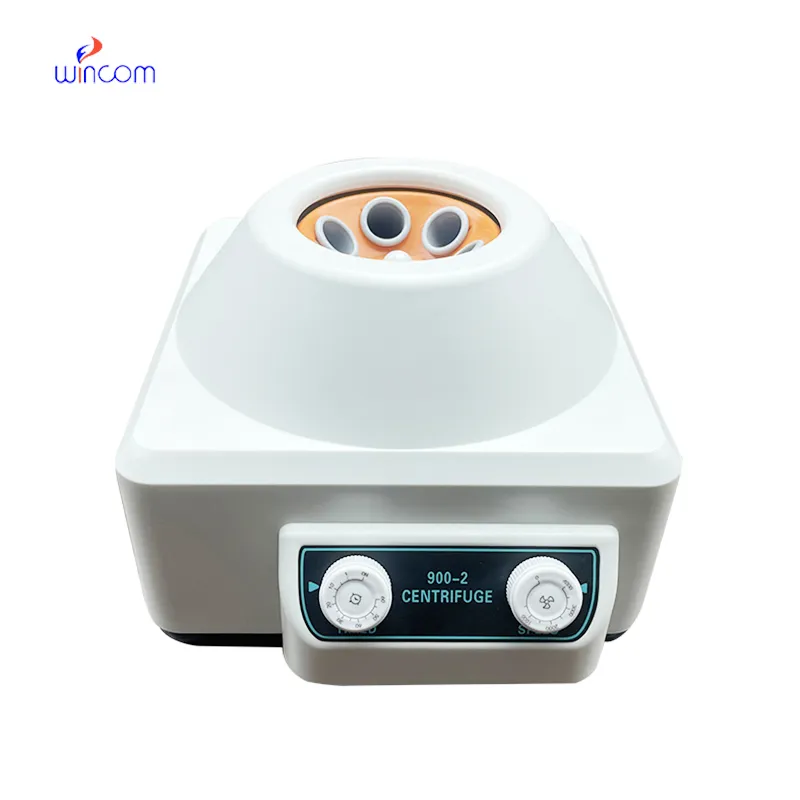
Routine maintenance of factory price large capacity refrigerated centrifuge begins with frequent cleaning and careful handling. Before each run, users should confirm that there are properly sealed, loaded tubes to prevent imbalance. The rotor, buckets, and seals should be washed gently and dried with air after each session. Periodic calibration checks ensure precise speed and temperature measurement. Rotor overloading is to be prevented since it will reduce motor life. With monitoring each maintenance cycle and adhering to safety protocols, laboratories can extend the functional life of factory price large capacity refrigerated centrifuge while ensuring precise performance.
A factory price large capacity refrigerated centrifuge is a universal gadget designed to separate parts in a mixture through sheer spinning power. A factory price large capacity refrigerated centrifuge operates through the principle of sedimentation, in which heavier particles move outwards and lighter particles remain at the center. Employed within laboratories, clinics, and industry in general, a factory price large capacity refrigerated centrifuge may be utilized to separate materials such as blood plasma, proteins, and chemical reagents with accuracy. Modern factory price large capacity refrigerated centrifuge exist in various forms, from benchtop to industrial types and ultracentrifuges, all for specialized applications. They are accurate and reproducible, a necessity in production and research.
Q: What is a centrifuge used for? A: A centrifuge is used to separate mixtures based on density differences by spinning them at high speeds, allowing heavier particles to settle away from lighter ones. Q: How does a centrifuge work? A: A centrifuge operates by generating centrifugal force, pushing denser materials outward while lighter components remain near the center, resulting in effective separation. Q: What are common applications of a centrifuge? A: Centrifuges are used in laboratories, hospitals, and industries for blood testing, chemical analysis, purification, and sample preparation. Q: How often should a centrifuge be calibrated? A: Calibration should be performed at least once a year or whenever performance inconsistencies appear to ensure accuracy and reliability. Q: Can a centrifuge handle biological samples? A: Yes, many centrifuges are designed for biological materials such as blood, plasma, and cell cultures under controlled and sterile conditions.
This ultrasound scanner has truly improved our workflow. The image resolution and portability make it a great addition to our clinic.
We’ve used this centrifuge for several months now, and it has performed consistently well. The speed control and balance are excellent.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
I’m looking to purchase several microscopes for a research lab. Please let me know the price list ...
Hello, I’m interested in your water bath for laboratory applications. Can you confirm the temperat...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko