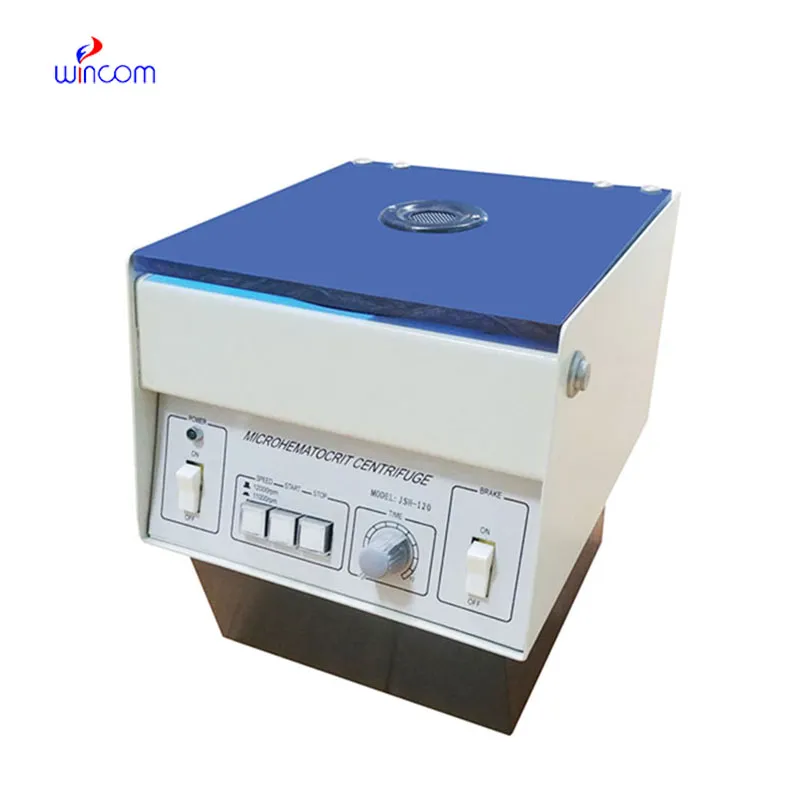
Crafted specifically for precision, the high speed refrigerated centrifuge wholesale is additionally improved by digital and mechanical enhancements. Intelligent balancing systems automatically eliminate unbalanced loads, improving performance as well as safety. Materials such as reinforced polymers and high-grade aluminum are becoming standard in rotor production, reducing wear and maximizing life in operation. Real-time sensors of temperature and speed offer feedback for reliable results. These developments not only improve separation efficiency but also allow for the achievement of stringent laboratory standards. With increasing research needs, high speed refrigerated centrifuge wholesale technology develops further to ensure better reliability and reproducibility.
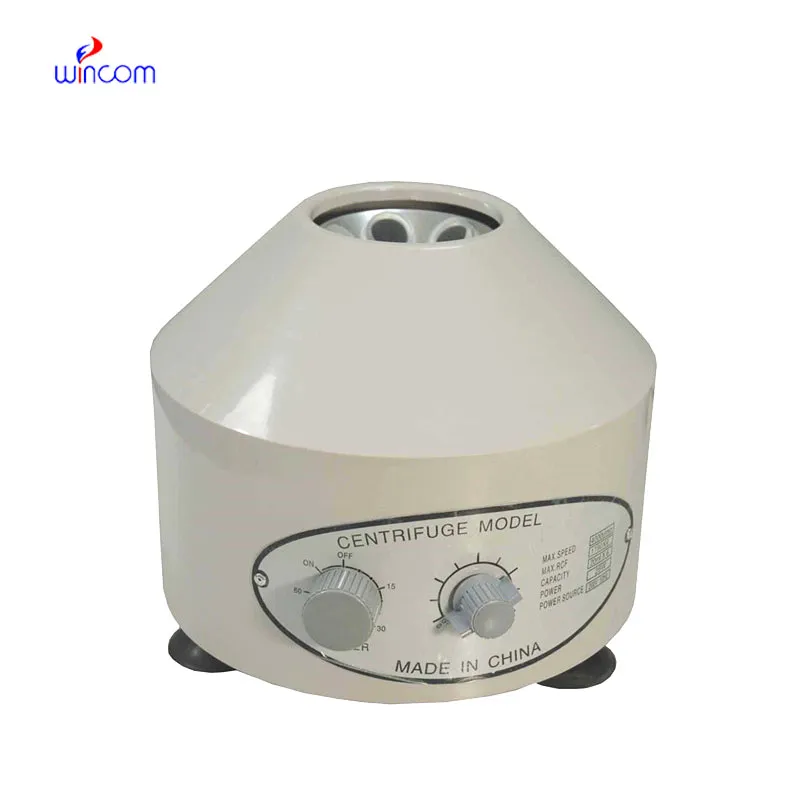
high speed refrigerated centrifuge wholesale are part and parcel of the functioning of modern laboratories and factories. Applications include cell culture harvesting, purification of enzymes, and waste handling. In oil processing, they facilitate hydrocarbon/water separation. Clinical laboratories depend on high speed refrigerated centrifuge wholesale for accurate diagnostic tests, and chemical industries use them to purify chemicals and recover active ingredients. They also hold great importance in educational research, where repetition and accuracy are necessary to experimentation. This wide application reveals the extent to which high speed refrigerated centrifuge wholesale continue to drive scientific and industrial advancement globally.
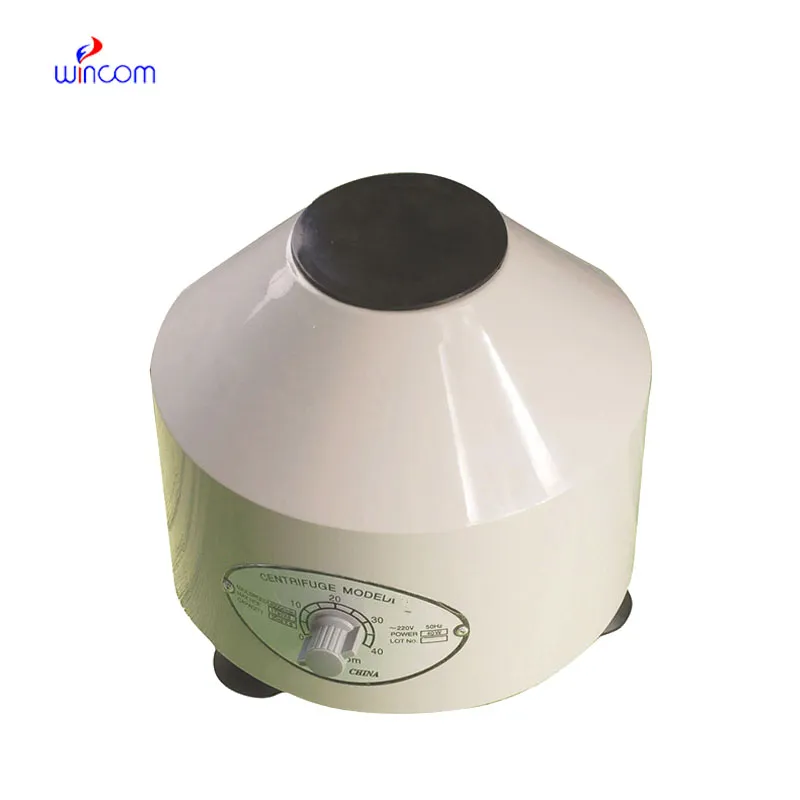
The high speed refrigerated centrifuge wholesale of the future will be innovative, intelligent, and integrated. With the advent of smart manufacturing, high speed refrigerated centrifuge wholesale systems will operate independently on predictive analytics. Programs with machine learning will interpret vibration patterns to optimize performance with minimal human involvement. Renewable energy integration will make operation more sustainable, and modular design will facilitate instant replacement of parts. Data visualization software will be more sophisticated, providing real-time feedback on the separation process. This blend of mechanical precision and intelligent technology will place high speed refrigerated centrifuge wholesale at the forefront of international scientific advancement.
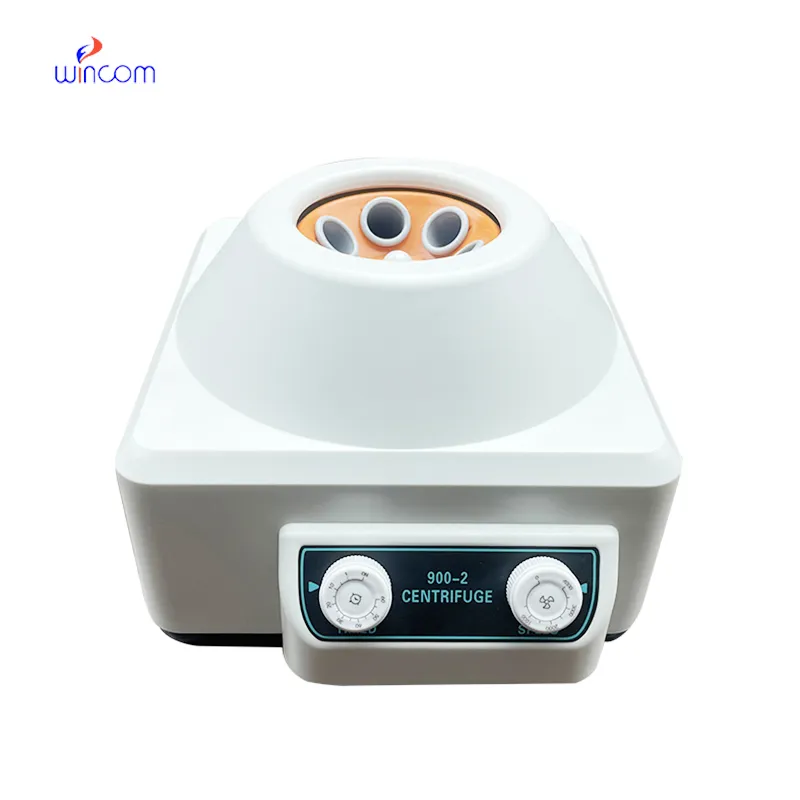
Well-maintained high speed refrigerated centrifuge wholesale assure trouble-free operation and optimize equipment longevity. Users must ensure balanced loading to prevent excessive stress to bearings. Regular cleaning of the rotor, chamber, and seals reduces cross-contamination. Regular lubrication and calibration ensure mechanical accuracy. Logs of maintenance, checklists, and other records facilitate quality control and inspection for compliance. Internal humidity and dust exposure should be reduced. Laboratories use preventive maintenance instructions to guarantee that high speed refrigerated centrifuge wholesale delivers constant high performance with little downtime and repair.
The high speed refrigerated centrifuge wholesale is an essential instrument in science and engineering. It is able to separate material constituents based on their differences in density by rotating them at very high speeds. In biotechnology, it is used to purify cells, DNA, and enzymes. In chemistry, it purifies liquids and removes impurities from them. high speed refrigerated centrifuge wholesale also play a crucial role in medical diagnosis when preparing blood samples. Their mechanical precision and regulation of speed ensure safe use. Constantly enhanced design and electronic monitoring system development enhances efficiency, and high speed refrigerated centrifuge wholesale are thus inevitable in numerous modern applications.
Q: How is a centrifuge different from a mixer or shaker? A: Unlike mixers or shakers that blend materials, a centrifuge separates components based on density through high-speed rotation. Q: What power requirements does a centrifuge need? A: Most benchtop centrifuges use standard AC power, while industrial units may require higher voltage for greater speed and capacity. Q: Can a centrifuge be used in pharmaceutical production? A: Yes, centrifuge equipment is widely used to purify chemical compounds and biological materials during drug manufacturing processes. Q: How do I prevent vibration during operation? A: Ensure all tubes are evenly loaded, rotors are clean, and the machine is placed on a stable, level surface. Q: What is the lifespan of a centrifuge? A: With regular maintenance and proper usage, a centrifuge can last for many years while maintaining consistent performance.
The microscope delivers incredibly sharp images and precise focusing. It’s perfect for both professional lab work and educational use.
The hospital bed is well-designed and very practical. Patients find it comfortable, and nurses appreciate how simple it is to operate.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
We’re looking for a reliable centrifuge for clinical testing. Can you share the technical specific...
We’re interested in your delivery bed for our maternity department. Please send detailed specifica...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko